BOILERS FOR PEOPLE THAT KNOW AND CARE®

LEARN MORE SEE THE INDUSTRIES WE SERVE LEARN ABOUT BOILER APPLICATIONS LEARN MORE VIEW OUR BOILER SOLUTIONS LEARN MORE

WHO WE ARE AND WHAT WE DO

Rentech Boilers is America’s leading and most trusted industrial boiler manufacturer. For over three decades, we have provided reliable, efficient boiler solutions tailored to the specific needs of each industry we serve.

CUSTOM BOILER SOLUTIONS BY INDUSTRY

Rentech provides custom designed, and engineered systems, to meet the specific needs of our clients. Combined with our large, cost-saving, shop assembly capabilities, and professional field services group, Rentech has become the preferred supplier of industrial boilers for clients across the U.S. and the world. 

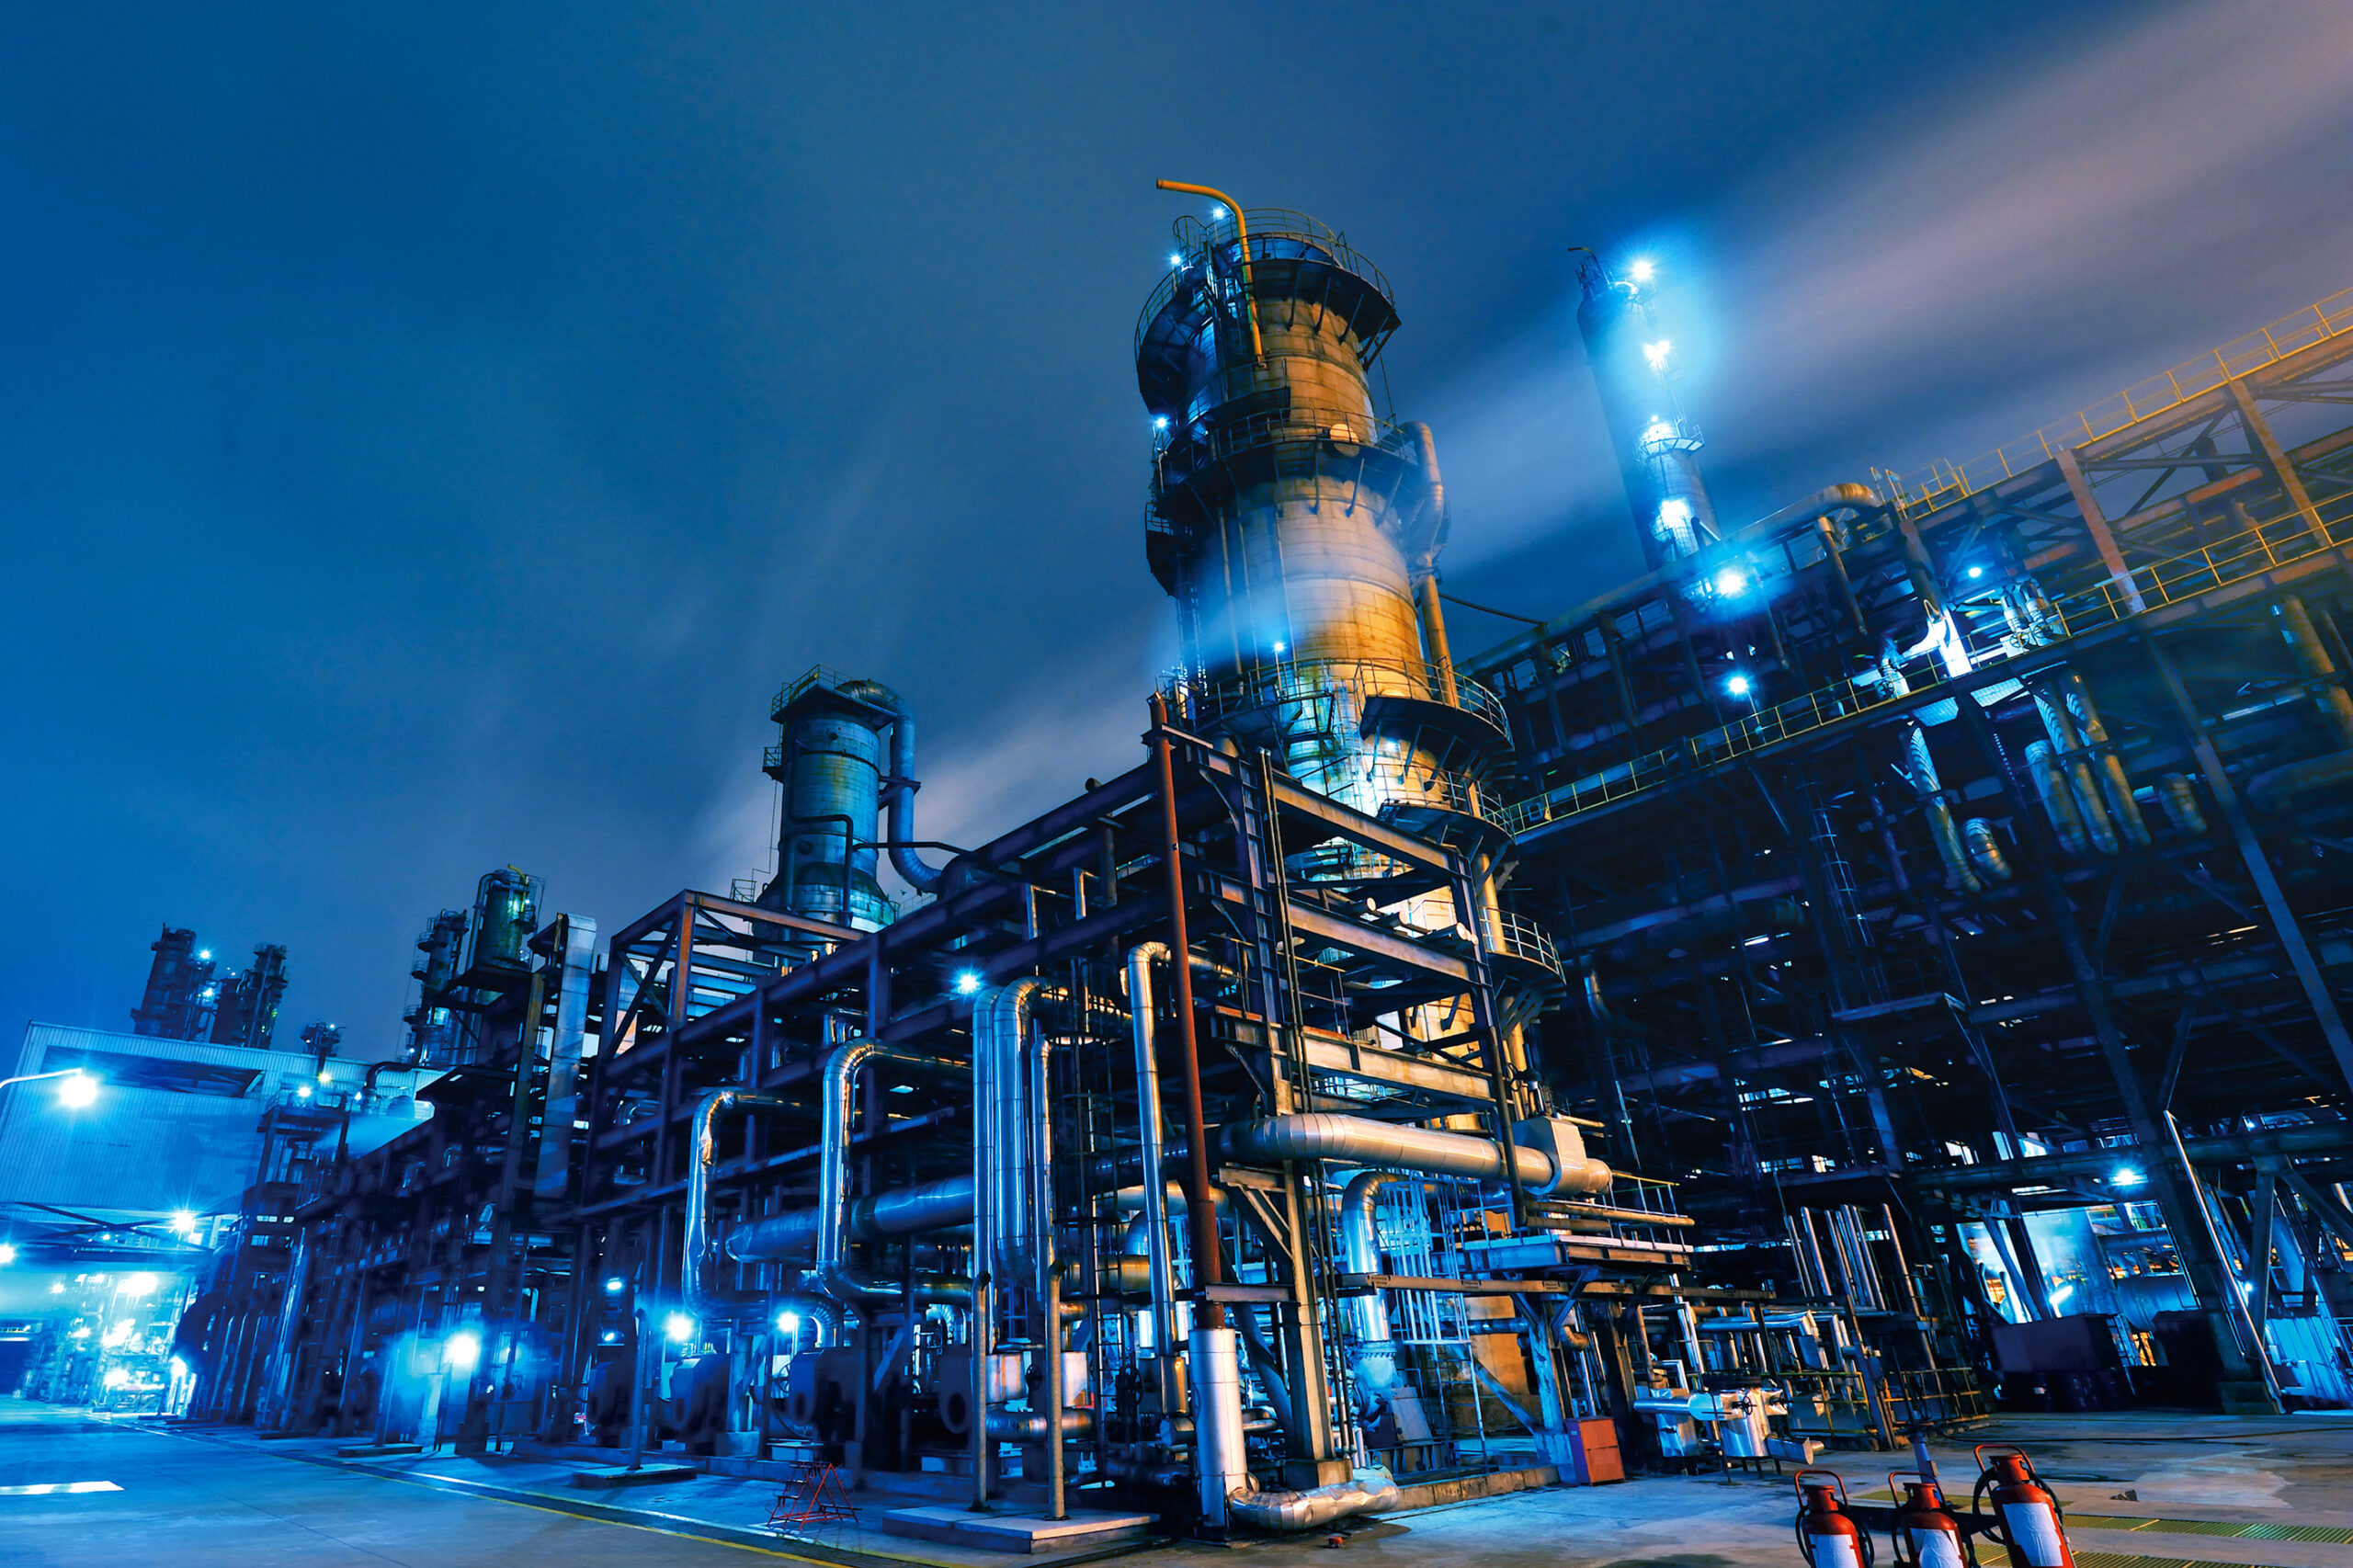
Membrane tube panel bending. CHEMICAL PLANTS REFINERIES Our watertube boilers are used in refineries as a part of the heat generation for the refining of crude oil. Heated steam helps distill the crude into its various components. ENERGY PRODUCTION From natural gas processing to upstream oil production,our fired watertube boilers & HRSGs are used in the SAGD, midstream and downstream process of refining raw materials. LEARN MORE > POWER GENERATION Our fired watertube boilers are commonly used as auxiliary boilers at power plant. Our HRSGs can be used to produce steam to drive steam turbines in power generating applications. LEARN MORE > Our waste heat watertube boilers are used to recycle waste heat in most chemical manufacturing processes. LEARN MORE > LEARN MORE > RENEWABLES Membrane tube panel bending. LEARN MORE > CARBON BLACK BREWERIES/DISTILLERIES Probably the most important piece of equipment in the distillation process, a steam boiler is critical to the creation of quality spirits. Our fired watertube boilers are perfect for this type of application. Our waste heat watertube boilers are used in the carbon black production process to cool the tail gases in order to implement required emission controls. Whether it is extracting ethanol from corn and soybeans, or converting solid waste to energy, our boilers are a key part of the process. Our boilers provide everything from central power plant services, campus heating and cooling, hot water generation, to laboratory sterilization applications. LEARN MORE > LEARN MORE > LEARN MORE > CAMPUSES SULFURIC ACID PLANTS Membrane tube panel bending. MINING MANUFACTURING Our boilers have long been a staple in a variety of manufacturing situations. From providing heat to being integral to the process, our boilers make things around the world. The process of mineral and metal extraction from the Earth requires heat, typically provided by a fired watertube boiler or and HRSG . Waste heat fire ube and waste heat watertube boilers are integral to the production of sulfuric acid. Boiler flue gases as well as steam and heat generated by boilers are a key part of the production process. LEARN MORE > LEARN MORE > LEARN MORE >

APPLICATIONS

Each Rentech Industrial Boiler is custom designed and engineered to meet specific client requirements, facility space, and application needs. Our boiler solutions support a wide range of applications, including the following.

PRODUCTS

Rentech Boiler Systems manufactures a wide range of industrial boiler solutions engineered to meet specific steam capacity, pressure, temperature, and application requirements from all heavy industries.

REPAIR AND SERVICE

Rentech delivers boiler repair and support services the same way as it builds their boilers. 

At Rentech, we believe our commitment to quality shouldn’t stop at manufacturing. That’s why our field service team brings real expertise to every boiler repair, rebuild, upgrade, or retrofit. Whether we’re working on-site at your facility or in our own fabrication shop, you’ll see the same attention to detail and focus on safety. Our engineers are hands-on partners dedicated to keeping your operations running without a hitch.